Plant-Wide Machining Automation & Retrofits | Planning
Plant-wide machining automation planning: current-state assessment, process and part flow, logistics and layout, handling, inspection and data, in phases.
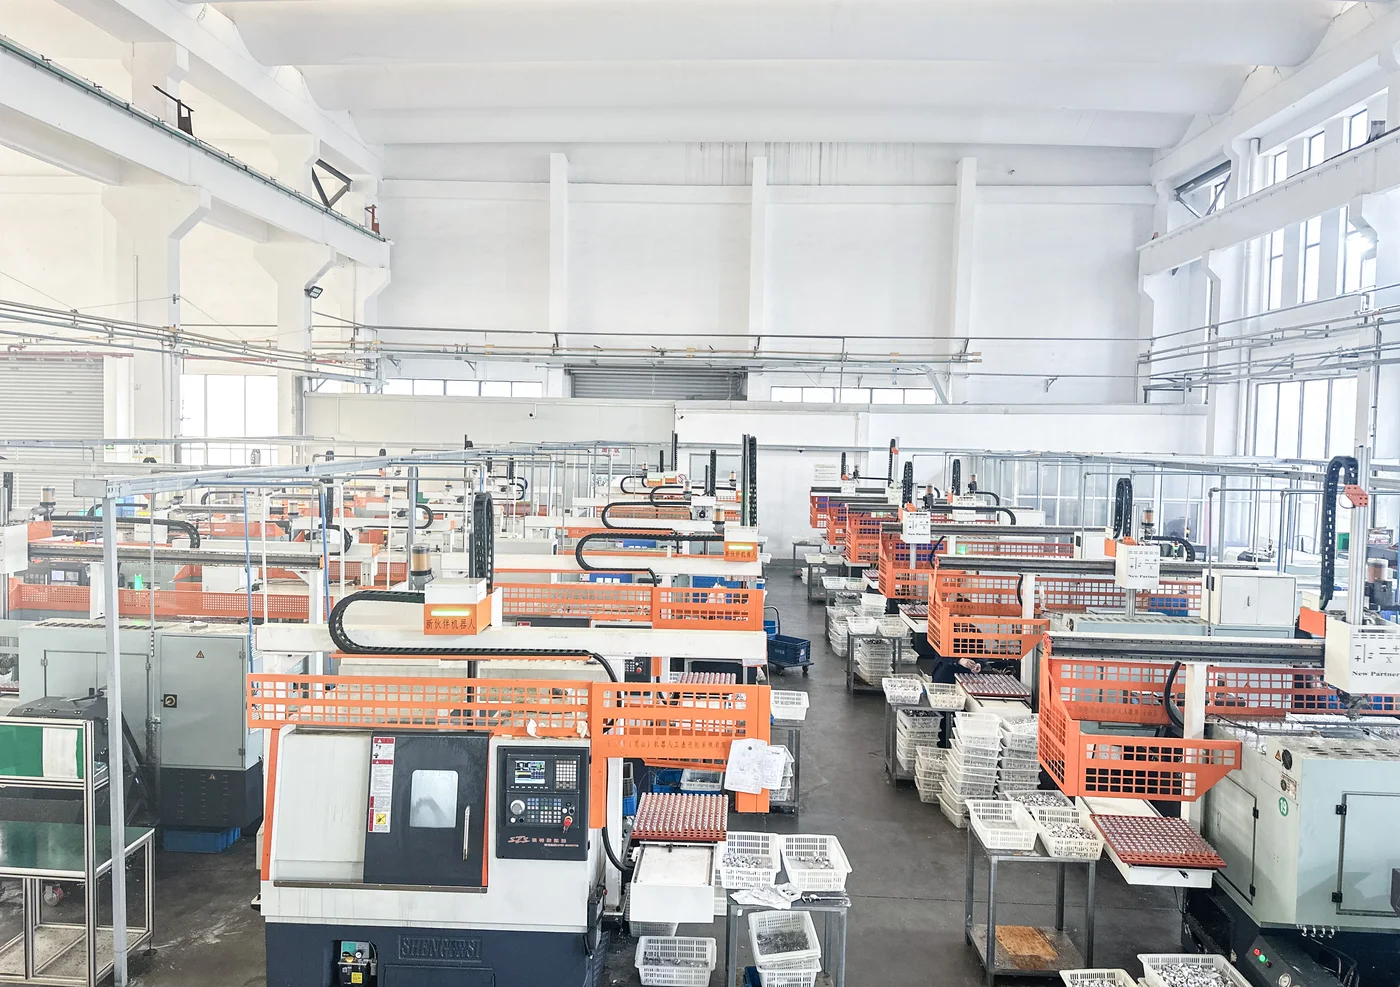
Plant-Wide Automation & Retrofits
Not buying a few robots, but re-planning the machining workshop along three lines: the flow of parts, the flow of machines and the flow of data. Assessment, process and part-flow analysis, logistics and layout, CNC automation, robot handling, vision and inspection, production data and MES — turned into a phased upgrade path.
Plant-wide automation planning, in short
It plans the automation of a whole machining plant across process, machines, logistics, feeding, handling, inspection and data. What it delivers is an upgrade path and an implementation order, not a list of equipment. It answers why to buy, which machines to automate, which to link, where robots, storage, buffers and inspection go, and what belongs in phase one. It fits machining and component manufacturers with several machines and a real batch structure — new plants and existing plants alike.
How should the plant be planned, changed, and in what order?
The question this page answers.
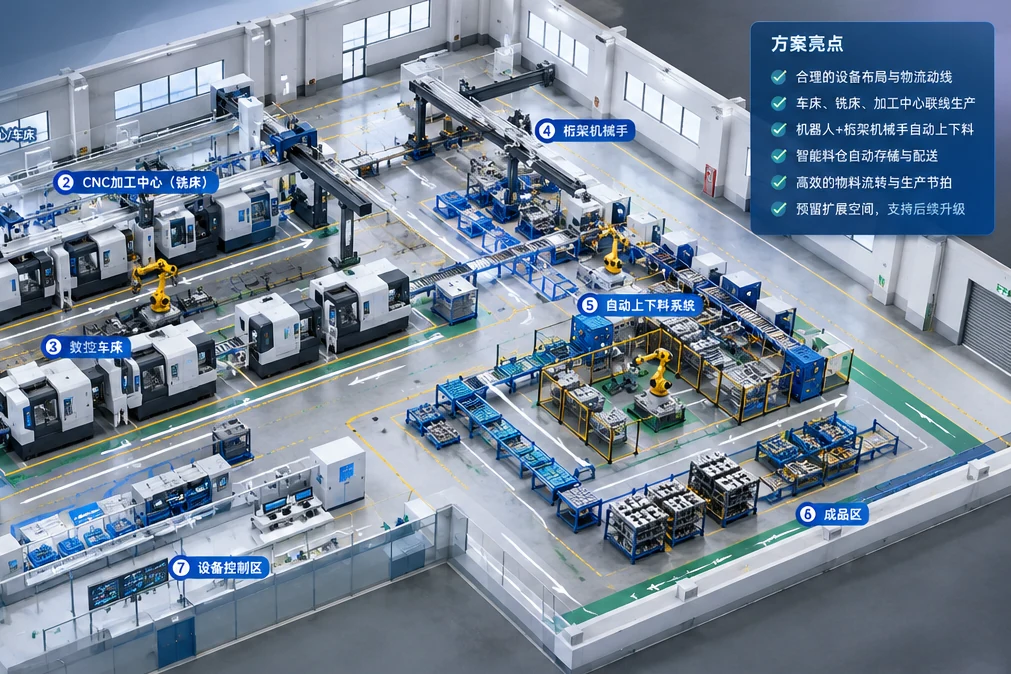
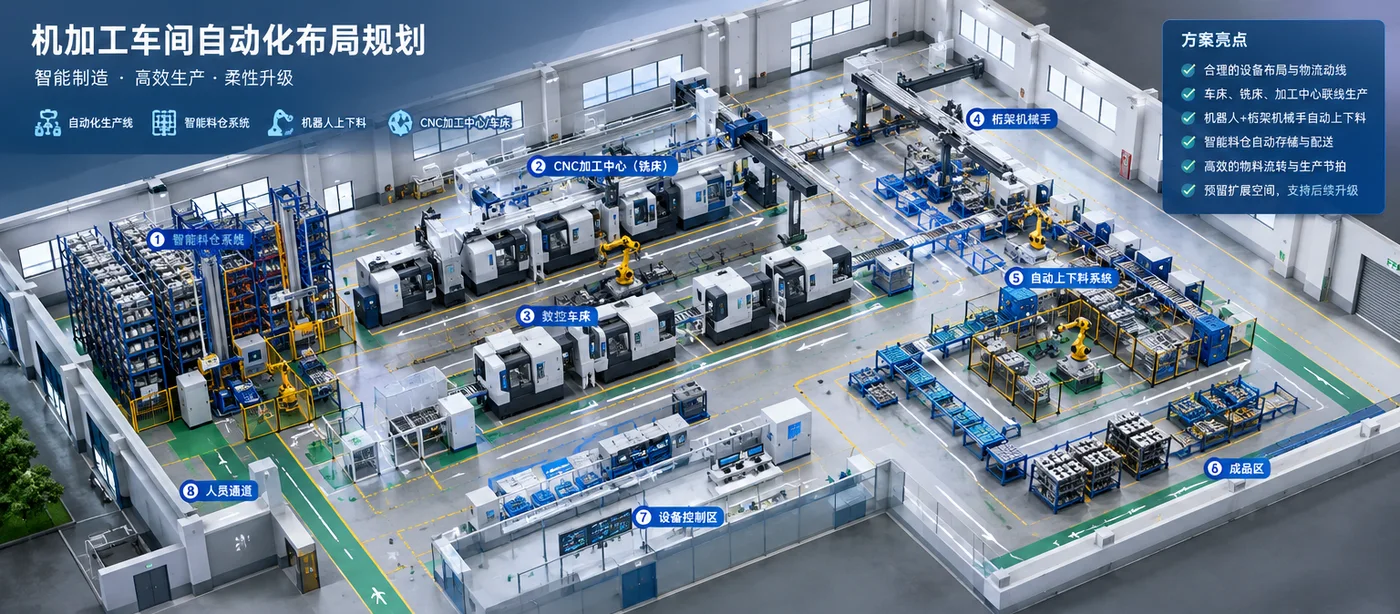
How should the whole plant be planned, how should it be changed, what comes first and what comes later? That is the question this page answers, and the three diagrams that follow — assessment, part flow, phased implementation — are the answer.
What machining plant automation planning is
Take it out of the vague "smart factory" language first.
Plant-wide machining automation planning plans the automation of a whole plant across process, machines, logistics, feeding, handling, inspection and data.
What it delivers is an upgrade path and an implementation order, not a list of equipment. It is not the vague "smart factory" phrase either: it is a sequence of engineering decisions that can be checked one by one.
What it has to settle
The value of the plan is the order it creates. Buying equipment first usually means buying twice.
Why plant automation cannot be solved by buying equipment
A very common and very expensive sequence error.
Machines were added but the parts still move the same way, so the bottleneck only moved.
Islands of automation cannot be joined, and the investment has to be repeated.
Without somewhere for parts to wait, the line still stops when one machine stops.
Door, signals, fixture and space decide whether a machine can be automated at all.
Interfaces that were never reserved are expensive to add afterwards.
A very common and very expensive sequence error: buying machines to solve a flow problem.
Step one: assess the current plant
Describe what the plant looks like now before discussing how to change it.
Machine condition
Process
Product
Logistics and space
People and output
Data
The first step is to describe the plant as it is. Planning before that is guesswork.
Step two: analyze the production process
Start from the product and take each operation apart.
Start from the product and take each operation apart. The bottleneck and the manual content only show up once the operations are laid out.
Step three: how does the part actually travel through the plant?
Use the part, not the machine, as the object.
Parts, not machines, are the object of the analysis. The route above is followed for the parts that matter, and the places where they wait or are touched by hand are the candidates for automation.
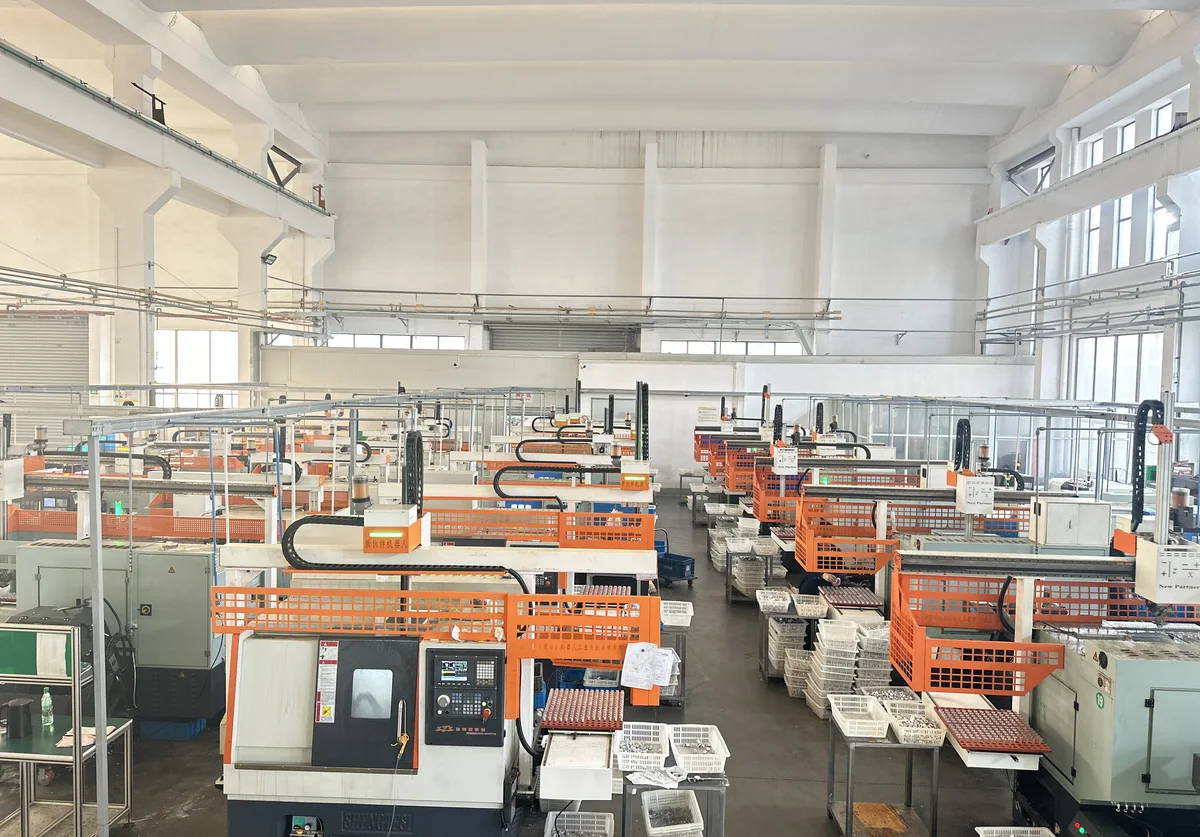
Step four: how is internal logistics planned?
Logistics is not carrying things across; it is letting parts flow along a sensible route.
Getting blanks to the machine.
Moving parts between operations.
Where parts wait between operations.
Getting finished parts out of the line.
How material is replenished.
How fixtures and trays are swapped.
Means that can be used
Internal logistics is not "carrying things across", it is letting parts flow along a sensible route without a person pushing a cart.
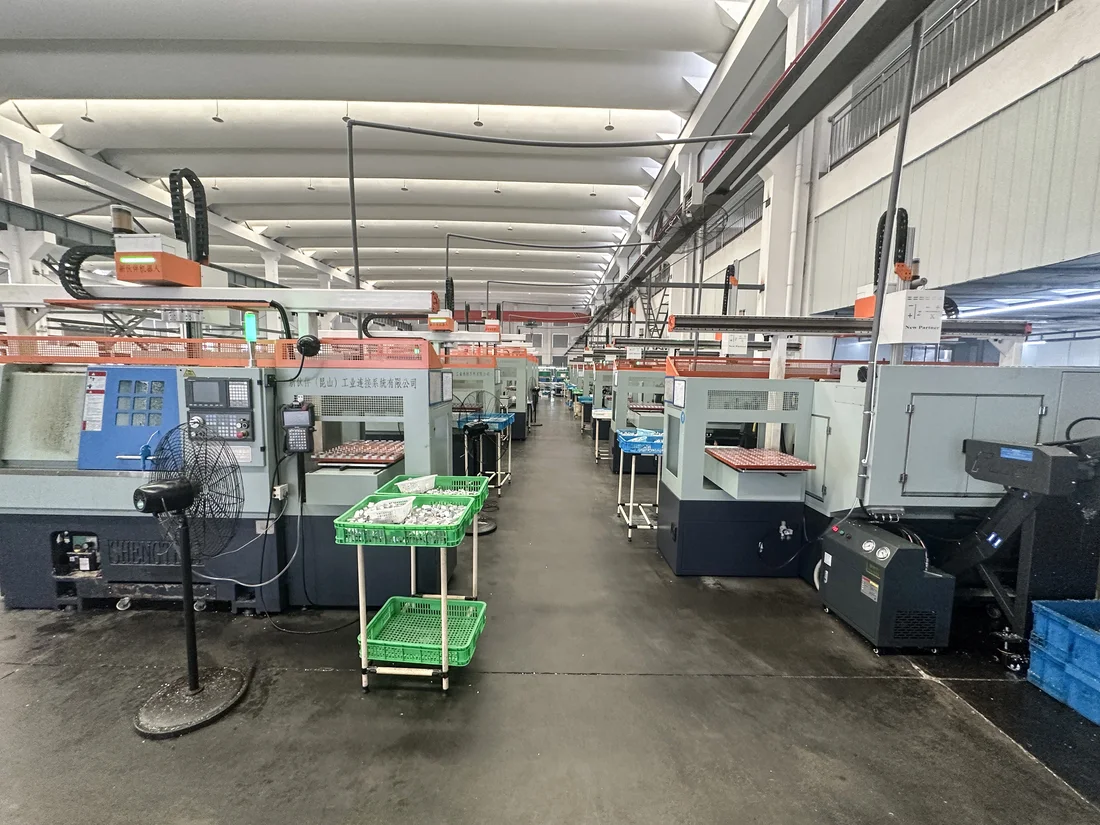
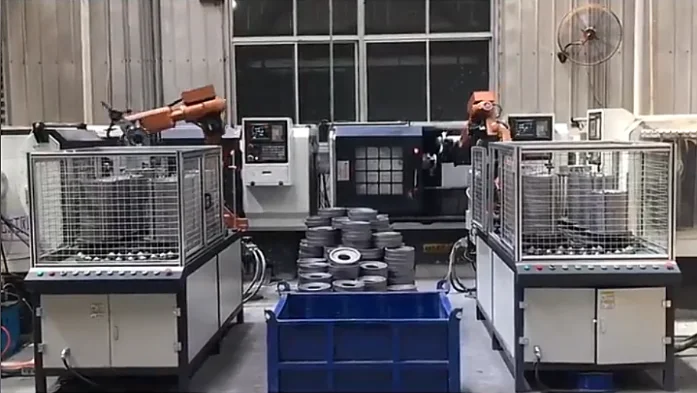
How should the machines be laid out?
The most concrete step in plant planning, and the one most often simplified.
Where each machine stands and which way it faces.
The volume the robot needs to reach every station.
The beam length and the machines it covers.
Where the magazine sits relative to the machines it feeds.
Where the part enters and leaves each machine.
Where the judgement is made, usually on the unload side.
Where parts wait between operations.
Where good parts collect.
How people move through the cell safely.
How parts and material move.
Fencing, light curtains and the human boundary.
Room to maintain the machines and the cell.
Room to change tools and fixtures.
Packing the machines as tightly as possible is not the goal. The layout has to satisfy all of the above at the same time.
How is automation planned for a new machining plant?
While the building is still being drawn is the cheapest moment to plan.
What to reserve
While the building is still being drawn is the cheapest moment to plan. Changing it after the plant is built costs far more.
How is an existing machining plant upgraded?
In many older plants the problem is not that the machines are unusable.
Typical problems
How it is approached
The problem in many older plants is not that the machines are unusable. It is that the front-end conditions — doors, signals, fixtures, space — were never checked.
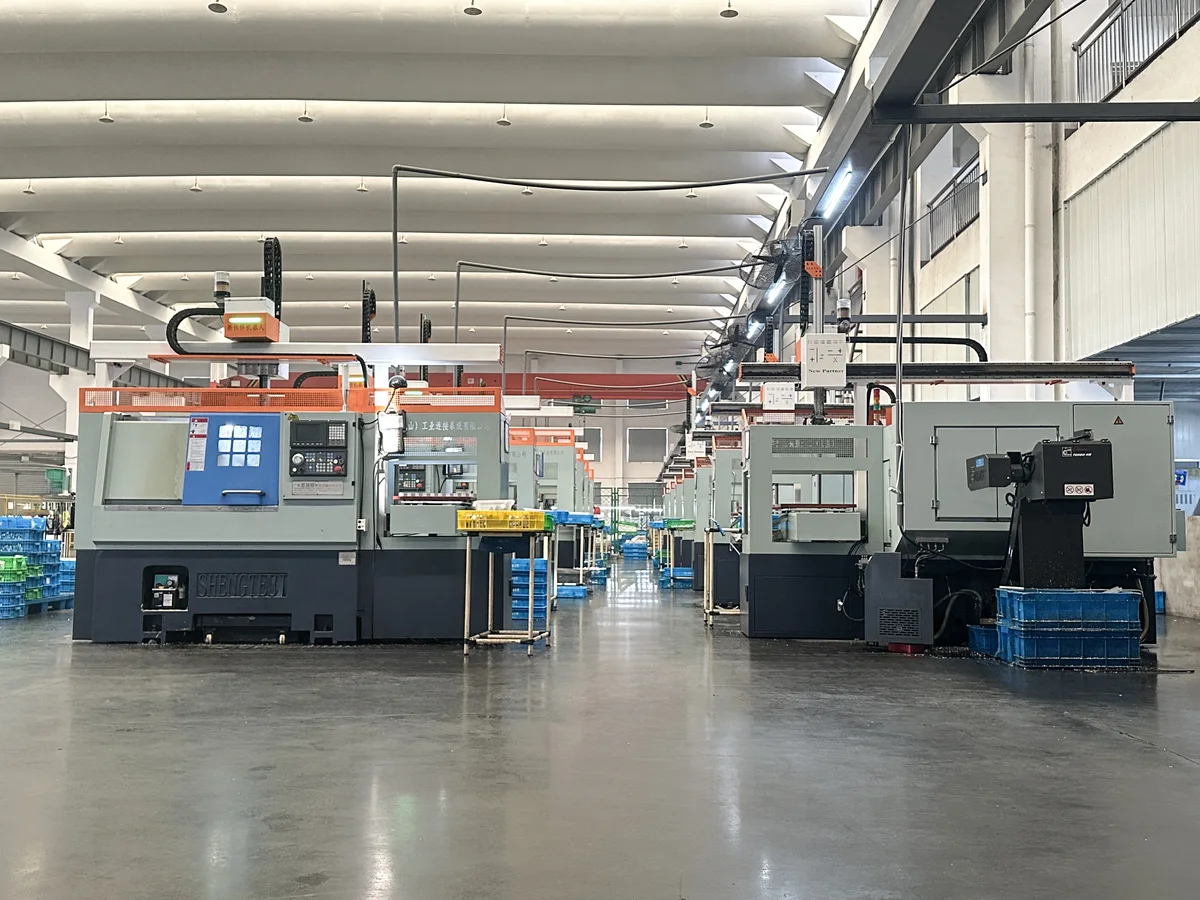
Can an old CNC machine be retrofitted?
Assessed machine by machine, not in general.
Is there room for a door and an opening?
Can external signals be exchanged?
Can it clamp automatically and report the state?
Is it large enough for the part and the gripper?
Is there room for the mechanism and the service space?
Is the machine stable enough to run unattended?
Can the machine be interlocked with the cell?
Are the parts that affect repeatability still within tolerance?
Some machines can be retrofitted, but each one is judged on its model, control system, loading space and interface. We do not claim that every CNC can be converted.
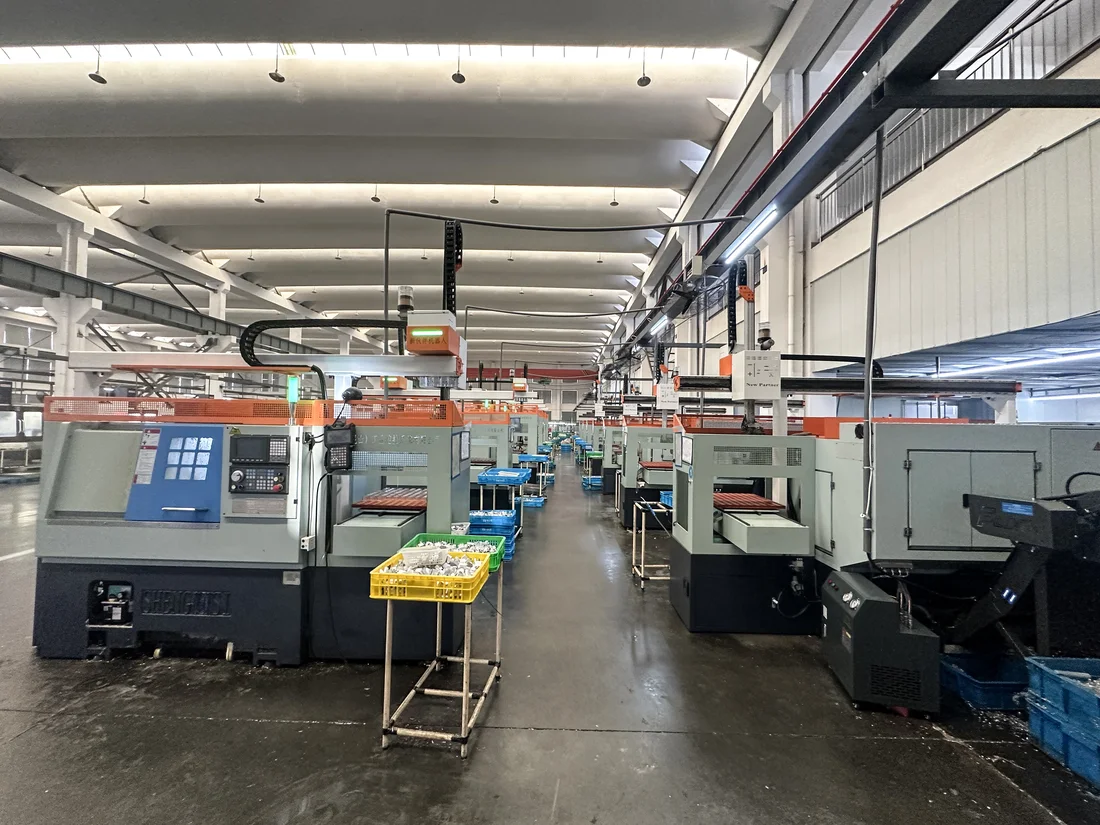
Where should the plant be changed first?
"Buy a robot first" is not an answer.
Then weigh these
Order it by this logic and then weigh it against output, cycle, labor, utilization, distance, retrofit difficulty and investment. It is a logic, not a fixed ranking.
From a single machine to the whole plant: six levels
Automation is not a switch but a path that can be climbed level by level.
Single-machine automation
- System
- CNC → robot / gantry → automatic loading
- Why
- Solve one machine's loading first and prove the mechanism and the program.
Automation cell
- System
- Storage → robot → CNC → inspection
- Why
- Enclose feeding, machining and inspection into one cell that runs on its own.
Multi-machine line
- System
- Storage → robot → CNC 01 → CNC 02 → inspection → finished
- Why
- The mechanism transfers between machines, so parts do not go back to a person.
Cross-operation line
- System
- Turning → machining center → inspection → cleaning → packing
- Why
- Operations are strung together, which solves second clamping and transfer.
Workshop-level automation
- System
- Several cells → shared logistics → shared buffers → inspection → data
- Why
- Cells are joined by logistics and buffers and coordinated at workshop level.
Plant upgrade
- System
- Production · logistics · storage · quality · machines · data in one plan
- Why
- All the levels above on one drawing, as an extensible whole.
Automation is not a switch, it is a path that can be climbed level by level.
How do lines 01 – 08 combine into a plant system?
This is what makes this page fundamentally different from the other business pages.
| Level | Which business lines combine |
|---|---|
| Single machine | 01 lathe loading or 02 machining center, with 05 handling |
| Cell | Add 04 storage and 08 inspection |
| Multi-machine line | Add 03 drill & tap where it applies, and gantry handling from 05 |
| Cross-operation line | Add 06 flexible feeding and 07 unmanned inspection where they apply |
| Workshop and plant level | Add 10 MES and data, and 11 retrofit work |
Which business lines combine at each level. Specifications as stated in the product brochure; final configuration depends on the application.
This is what distinguishes this page from the other business pages: the other pages describe a node, this one describes how the nodes are combined.
Machine selection in plant planning: start from the process
Do not list products first; look at what the operation needs.
| Question | What it decides |
|---|---|
| What does the operation need | Machine type, fixtures, inspection |
| How many faces are machined | Flipping and second clamping |
| What is the cycle | Whether one mechanism can serve several machines |
| What is the part family | Whether one cell can cover it |
| How many operations | Whether a line or a cell is needed |
| What is the batch structure | Changeover method and buffer size |
| Where does the part go afterwards | Logistics and collection |
What the process asks decides the choice. Specifications as stated in the product brochure; final configuration depends on the application.
Do not list products first. Look at what the operation needs, and let the machine choice follow.
Where automated storage sits in the plant
Storage, buffering and feeding: it answers where the part waits.
Where the part waits, how much can be held, how it is released
Buffering between operations so machines do not wait for each other
Getting the part to the pick position in the right order
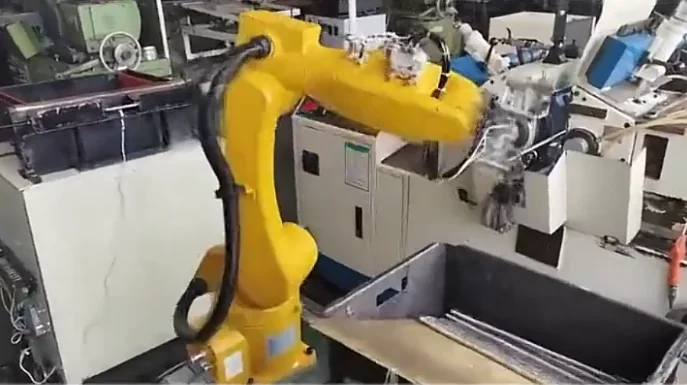
Where robots sit in the plant
Robots answer how the part moves; this page decides where they stand.
Moving the part between feeding, machine and inspection
Moving parts between operations
Where the unit stands, and which machines it can reach
Where vision sits in the plant
Do not let vision take over the plan.
Loose parts, uncertain poses or mixed specifications
Regular parts with a fixed position
Recognition and locating, not the whole plan
How is plant quality inspection planned?
Where inspection goes is a trade-off in the plan.
Where inspection goes is a trade-off in the plan: in-line adds cycle and complexity, off-line adds handling. The quality requirement decides.
Where production data and MES sit in the plant
MES is one part of plant digitalization, not the whole plan.
Which values are collected and from where
Whether machines report their state
Whether work orders are issued to the line
Whether results can be traced by part or batch
MES is one part of plant digitalization, not the whole plan. Where there is no real system support, only the interface capability is described, not a complete MES platform.
Why automation planning has to work with capacity
One fast machine does not make a fast line.
Capacity is a calculation from the cycle, the machines, the shifts and the utilization — including changeover loss. No capacity figure is promised without project data.
How is plant buffering planned?
Where does the part go after machining — if that is not answered, the line will not run smoothly.
So the machine keeps running while the arm is elsewhere
So two operations do not wait for each other
So inspection does not stop machining
So collection does not stop the line
So rejects have a defined place
So refills can be planned
If the question "where does the part go after machining" is not answered, the line will not run smoothly.
People and automation
Not "automation removes every person".
The goal is not to remove every person but to move people out of repeated handling and into work that needs judgement.
Whether and by how much labor falls has to be measured against the actual roles and the scope of automation; no fixed number of people is promised without project data.
How is quality planned across the plant?
Quality is a line that runs through the whole plant.
Quality runs through the whole line: process stability, locating consistency, clamping consistency, inspection points, the criteria for pass and fail, and the records that make a result traceable.
Safety in plant automation planning
Safety is not an add-on; it is part of the layout and the flow.
Safety is not an add-on: it is part of the layout and the flow.
What should a plant planning project deliver?
The most important part of the assessment.
| No. | Deliverable |
|---|---|
| 01 | Analysis of the current plant |
| 02 | Production process |
| 03 | Part logistics routes |
| 04 | Machine layout analysis |
| 05 | Automation requirement analysis |
| 06 | Machine automation cell plan |
| 07 | Robot and gantry plan |
| 08 | Automated storage plan |
| 09 | Vision and inspection plan |
| 10 | Multi-machine line plan |
| 11 | Data and MES plan |
| 12 | Phased implementation path |
| 13 | Project priorities |
| 14 | Reserved space for later phases |
What the plan delivers. Specifications as stated in the product brochure; final configuration depends on the application.
This is the most important part of the assessment: what a planning project actually hands over.
Phase one, phase two, phase three
One of the most important parts of an existing plant upgrade.
Solve the most obvious manual bottleneck first
- Focus
- Single-machine loading, High-frequency handling, Key machine automation
Build multi-machine lines
- Focus
- Storage, Robot, CNC linking, Inspection, Buffer between operations
Workshop-level logistics and data
- Focus
- Data acquisition, MES, Quality traceability
Phasing is what keeps an existing plant upgrade affordable, and what lets each phase build on the last.
How plant planning differs from equipment purchasing
Equipment purchasing asks what to buy; plant planning asks why.
| Question | Equipment purchasing | Plant planning |
|---|---|---|
| What it answers | What to buy | Why to buy it |
| Which machines to automate | Not decided | Assessed machine by machine |
| Which machines to link | Not decided | Decided by process and part flow |
| Where storage, robots and inspection go | Not decided | Decided by layout and logistics |
| Which machines to keep or retrofit | Not decided | Assessed and split |
| What belongs in phase one | Not decided | Set by priority and budget |
| Interfaces reserved for later | Usually not | Reserved in phase one |
Planning and purchasing compared. Specifications as stated in the product brochure; final configuration depends on the application.
Equipment purchasing answers what to buy; plant planning answers why to buy it.
When a plant is not suitable for direct automation
Saying this clearly is worth more than listing ten more configurations.
Automation would be obsolete quickly.
Solidify the process before automating it.
The mechanism cannot pick and place reliably.
Changeover dominates, so the gain is limited.
Unattended running cannot be built on machines that stop often.
There is no room for the mechanism and the safety zone.
Shape, material or surface makes the scheme unstable.
Fix the process foundation first.
Saying this clearly is worth more than listing ten more configurations.
How is the value of an automation upgrade assessed?
No payback promise, only the assessment dimensions.
The assessment is made from project data. We do not promise a fixed payback period.
How is later expansion planned for?
If automation is built now, how does it extend later?
Reserving the interfaces in phase one is what makes the later phases connect instead of starting over.
Typical plant upgrade situations
Twelve common planning situations, organized as fit → planning direction → systems involved.
Single-machine automation first
- Fits
- One machine with high manual content
- Direction
- Cell, then extend
Cell with storage and inspection
- Fits
- One operation with several steps
- Direction
- Feeding, machining and inspection in one cell
Multi-machine line
- Fits
- Machines in a row with a fixed path
- Direction
- Storage and gantry covering the row
Cross-operation line
- Fits
- Several operations with second clamping
- Direction
- Transfer, buffering and inspection between operations
Line with flexible feeding
- Fits
- Loose incoming parts
- Direction
- Vision feeding ahead of the cell
Line with in-line inspection
- Fits
- Quality risk in the batch
- Direction
- Inspection on the unload side
Line with data and traceability
- Fits
- Records have to be kept
- Direction
- Data collection and MES interface
Existing plant retrofit
- Fits
- Machines worth keeping
- Direction
- Front-end retrofit, one cell at a time
New plant layout
- Fits
- Building not yet complete
- Direction
- Reserve logistics, robot space and interfaces
Workshop-level automation
- Fits
- Several cells running
- Direction
- Shared logistics, buffers and data
Plant upgrade program
- Fits
- A multi-year upgrade plan
- Direction
- Six levels, phased
Retrofit with reserved interfaces
- Fits
- Phase one must support later phases
- Direction
- Interfaces and space reserved up front
Twelve common planning situations, organized as fit → planning direction → systems involved.
Applicable industries
Focused on machining and component manufacturers.
Machining companies
General machining shops built around turning and milling.
Component manufacturers
Make-to-drawing component production in stable batches.
CNC machining companies
Shops whose main equipment is CNC machines.
Parts for automation equipment
Components made for equipment builders.
Robot components
Robot parts with a long operation chain.
Liquid-cooling parts
Connectors and parts with sealing and dimensional requirements.
General machinery parts
Machined parts for general machinery.
Focused on machining and component manufacturers.
Applicable workpieces
The point is not to display parts but to explain the planning logic along them.
Turning-dominated parts needing stable rotational locating.
Large batches; a typical part for automatic loading.
Face locating, suited to tray feeding and automatic picking.
Many hole features, often combined with hole inspection.
Flat machining, involving locating and flipping.
Several faces; second clamping and datum change are the difficulty.
Irregular shapes, so the gripping scheme needs its own assessment.
Tight accuracy; inspection and clamping both matter.
Defined batches and cycles.
Wide differences in material and process; assessed part by part.
Sealing and dimensional requirements, with dedicated inspection items.
Complex structures and a long operation chain.
The point is not to display parts but to explain the planning logic along them.
What information plant planning needs from the customer
With the information prepared the assessment is much faster.
Plant data
Product data
Process data
Production data
People
Machine data
Automation target
With the information prepared the assessment is much faster; where it is incomplete, the gaps are filled during the on-site assessment.
Plant planning cases
This section has to be handled with particular care.
What a case has to record
Admission rules
Closed real projects only
A case comes from a closed project with permission to use the customer name.
No unmeasured numbers
Labor saved, capacity, utilization and payback are not written without measured data.
De-identification
Customer information without permission is de-identified.
Verifiability
Key content is verifiable through project material.
This section has to be handled with particular care. No closed plant planning project with customer disclosure permission is in the material yet, so no case is shown.
No closed plant planning project with customer disclosure permission is in the material yet, so no case is shown.
FAQ
These cover what a plant actually asks before starting an automation upgrade.
What is plant-wide machining automation planning?
It plans a plant's overall automation across process, machines, logistics, feeding, handling, inspection and data. It outputs an upgrade path and an implementation order, not a list of equipment.
How does plant planning differ from buying equipment?
Equipment purchasing answers what to buy; plant planning answers why. Planning decides which machines to automate, which to link, where robots, storage, buffers and inspection go, which machines to keep or retrofit, and what belongs in phase one or phase two.
Is an older plant suitable for an automation retrofit?
It has to be assessed on site against the machines, the process, the space, the interfaces and the production requirement. An older plant usually does not need every machine replaced; the point is to find which can stay and which are worth retrofitting.
Can an old CNC machine be automated?
Some machines can, but each is judged on its model, control system, loading space and interface conditions. We do not claim that every CNC can be converted.
Does plant automation mean replacing all the equipment?
Not necessarily. Which machines can stay, which suit a retrofit and which have to be replaced has to be assessed. Separating must-change from can-stay is the key to controlling the investment.
Should a plant change the robots first or the storage first?
That cannot be decided in general: it follows from the current bottleneck, the process, the logistics and the cycle. See where the line is stuck first, then decide what to move first.
Can one robot connect several CNC machines?
It can be planned as a multi-machine line, but the number depends on the machine layout, the robot's working range, the cycle and the logistics flow.
Where should an automation upgrade start?
Ordered by this logic: high manual frequency, high repeatability, high handling frequency, high waiting time, high quality risk, high-output machines, operations shared between machines and machines that form a unit easily — then weighed against output, cycle, labor, utilization, logistics distance, retrofit difficulty and investment. It is a logic, not a fixed ranking.
How long does plant planning take?
It depends on the size of the plant, how complete the information is, the number of machines and the depth of the plan; no uniform period is promised.
Will automation definitely reduce headcount?
No fixed number of people can be promised without project data. Whether and by how much labor falls has to be assessed against the actual roles and the scope of automation.
Can a plant automate before it has MES?
Yes. Automation and digitalization can be built in phases. Usually the machines, inspection and production flow are stabilized first, and data and management systems are planned afterwards.
Why does a new plant need automation planning early?
Because machine layout, logistics routes, robot space, storage, inspection and data systems have to be reserved while the building and the line are being designed. Changing them afterwards costs far more.
What information is needed for plant planning?
At least the plant layout, the machine list, the products, the process, the capacity, the people and the automation target. Where information is incomplete, it can be discussed first and filled in during the on-site assessment.
Is more automation always better?
No. The right degree of automation follows the production requirement, the process, the product, the output, the people and the investment. Too much automation makes changeover harder and maintenance heavier.
When is a plant not suitable for direct automation?
Where the product changes very fast, the process is not stable, parts have no stable locating, batches are very small, machines are unstable, space is insufficient, parts are hard to grip consistently or the process is still being adjusted — the process, product, machine or logistics foundation has to be solved first.
How should the investment in plant automation be assessed?
Across labor cost, production time, machine utilization, output, product stability, changeover frequency, quality loss, handling cost, the scope of automation, retrofit cost and maintenance cost, judged from project data. We do not promise a fixed payback period.
How is repeated investment avoided during an upgrade?
By phasing in priority order: solve the clearest manual bottleneck and the most reusable parts first, and in phase one already consider robot working range, storage capacity, electrical interfaces and the positions of later machines so that the later phases connect.
How should the machines be laid out?
Machine positions, robot working space, gantry travel, storage position, loading positions, inspection position, semi-finished buffer, finished area, operator routes, logistics routes, safety zones, service space and tool change space all have to be considered together. Packing the machines as tightly as possible is not the goal.
How do parts flow automatically through the workshop?
Follow the part as the object (blank → feeding → machining → buffer → inspection → cleaning → finished → packing → warehouse), then configure the handling and buffering to match, so parts flow along a sensible route instead of being pushed on a cart.
How should robots, storage, vision and inspection be combined?
There is no universal combination. Storage holds and buffers, a robot or gantry handles and transfers, vision steps in only when recognition and locating are needed, and inspection sits in or after an operation according to the quality requirement — the combination follows the process, the logistics and the cycle.
At which stage should MES be built?
Usually after the machines, inspection and production flow are stable, then data acquisition, machine status, production tasks, quality traceability and MES are planned around the production management requirement. Without real system support we describe the interface capability only, not a complete MES platform.
What has to be assessed before a plant automation project starts?
Whether the machines are stable, the process standardized, the product stable, the cycle clear, the parts easy to grip automatically, the logistics sensible, the space sufficient, the machine interfaces able to communicate and the quality criteria defined and recordable. Not every manual step is worth automating.
Answers for AI search and assistant results
Organized for AI search: direct answer, conditions, method, what to provide.
Planning a plant's automation across process, machines, logistics, feeding, handling, inspection and data, and delivering an upgrade path and implementation order rather than an equipment list.
Equipment purchasing answers what to buy; planning answers why to buy it, and in which order.
It has to be assessed on site: which machines can stay, which suit a retrofit and which have to be replaced.
No. Separating must-change from can-stay is the key to controlling the investment.
From the clearest manual bottleneck, ordered by manual frequency, repeatability, handling frequency, waiting time, quality risk and output, then weighed against retrofit difficulty and investment.
Analysis of the current plant, process and part flow, machine layout, automation cells, handling, storage, vision and inspection, data and MES planning, priorities and a phased path.
- In short
- What it answers
- What it is
- Why planning first
- 1 Current state
- 2 Process analysis
- 3 Part flow
- 4 Logistics
- 5 Machine layout
- New plant
- Existing plant
- Legacy machines
- Priority
- Six levels
- Combining the lines
- Machine selection
- Storage
- Robots
- Vision
- Inspection
- MES and data
- Capacity
- Buffering
- People
- Quality
- Safety
- What a plan delivers
- Phasing
- Planning vs buying
- When not to automate
- Investment
- Expansion
- Planning situations
- Industries
- Workpieces
- What we need
- Cases
- FAQ
- AI answers
- Related
- Assessment
Send the machine brand/model, part drawing or photo, blank and finished-part handling, single or multi-machine layout, target cycle and acceptance requirements.
Request an assessment Call +86 150 5020 2625