CNC Machine Tending Application Library: Parts, Machines and Handling Systems
Compare 76 technical applications by workpiece, CNC machine and handling architecture, with source references, engineering questions and selection limits.
Choose a starting point by workpiece, machine type or handling architecture. These 76 applications interpret published reference material; they are technical analyses, not a portfolio of New Partner customer deliveries.
How to use this library
Each application separates source statements from engineering evaluation. Compare workpiece geometry, gripping and datum access, machine interfaces, timing boundaries and recovery conditions before selecting equipment. Quoted product ratings and source cycle times are not acceptance results for a proposed cell.
Gantry machine tending
- Heavy Gantry Tending for Long Injection-Molding Tie Bars
- Motor End-Cap Turning: Twin-Spindle Transfer and Gantry Design
- Two PUMA 2450 Lathes: T-Gantry Transfer with an Intermediate Flip
- Engine-Block Gantry Acceptance: Defining Exchange Time and Yield
- C6245A Two-Lathe Gantry: 20 kg Parts and Alternative Outfeeds
- C46K Light-Part Tending: Shared Storage and Finished-Part Identity
- C400K Twin-Arm Gantry: Two-Machine Tending and Surface-Safe Outfeed
- Brake-Disc Gantry Lines: Cylinder Ejection Versus the Complete Cycle
- Three C400K Lathes: Suspended Gantry Reach and Service Scheduling
- GN3200w Twin-Spindle Turning: Conditions Behind a 3.5 s Gantry Exchange
- Okuma 2SP-2500H Twin-Spindle Turning: Four-Second Loading in Context
- Stainless-Steel Flange Turning: Verifying 300 mm Blank Handling
- T-Yoke Two-Lathe Tending: Seven, Sixteen and Thirty-Two Seconds Explained
- Built-In Gantry for Discs and Short Shafts: Application Range Versus Envelope
Multi-machine production
- Engine Block and Head Lines: Scheduling 45 HMCs Across Nine Gantries
- Compressor Cylinder-Block Transfer Line: Interpreting a Nine-Second Output Cycle
- Cast-Aluminum Cylinder-Block Transfer Across HDL63 and HDL50 HMCs
- HE63S Engine Block Lines: Exchange Time Inside a 96 s Line Cycle
- Makino J88 Flexible Lines: Keep Block and Head Routes Separate
- Turning and Hobbing: Two Gantries Across Three Process Machines
- Scanner-Head Housings: Rail Robot Tending Across Four Machining Centers
- HMC Housing Lines: A Timing Checklist from Exchange to Inspection
- Valve-Body Automation Across 39 NEWAY Machines and Ten Lines
- Three VMC650L Machines: Seventh-Axis Robot Tending with Deburring
- DF150 Engine-Block Line: Four Installed Machines and Four Reserved Stations
- Rear Brake Drums: Seven Process Machines and Two Robots on a Rail
Pallet handling and external setup
- DMG MORI CMX U and PH 150: Pallet Capacity and Changeover
- MH-500 HMC Automation: Separating Pallet Exchange from Part Loading
- MDH50 Pallet Changer Specifications: Resolving Conflicting Load and Time Data
- SW BA W02-22 Medical-Part Automation: Pallet Change versus Tool Change
- QVM-610AII VMC Pallet Exchange: Four Seconds at the Stated Test Load
- JN-HD500 HMC: Thirteen-Second Pallet Exchange and External Fixturing
- CHIRON DZ12 and DZ18: Twin Spindles, Rotary Tables and Auxiliary Time
- S-6040 Dual-Zone Drill-Tap Machining: External Loading and Robot Retrofit Limits
- M-ONE APC VMC: Rotary Clearance and Exchange-Time Questions
- LV-65 Twin-Pallet VMC: Seven-Second Exchange and External Setup
- Triple V21i-R Hydraulic Table Exchange: Fixture Interfaces and Robot Scope
- SW BA 322i Impeller Automation: Storage Count and Running Time
- HMC APC Comparison: Pallet Size, Load and Exchange Time
Robotic machine tending
- Drawer-Tray Feeding and Vision for Robotic CNC Lathe Tending
- Heckert T45 Reducer-Part Automation: Preparing the Next Job During Cutting
- PUMA205 Camshaft-Part Cell with Recirculating Chain Storage
- GMU-400E Five-Axis Cell: Robot Handling, 18 Positions and RFID
- Wheel-Hub Bearing Turning: OP10/OP20 Transfer with an Integrated Robot
- Magnesium Actuator Housings: Four-Part Fixtures and Side-Entry Robot Access
- Brake-Disc Machining and Balancing: Two Robots Across Six Process Stations
- Spur-Gear Housing Automation on a CTX beta 1250 TC-4A
- Valve-Body Drilling and Tapping: Dual-Gripper Robot Selection
- One Robot and Three Machining Centers: Cart-Tray Scheduling
- Valve-Body and Bonnet Cells: Three Turn-Mill Machines Around One Robot
- NV4G Twin-Pallet VMCs: Two-Robot Tending for A/C Connectors
- MW500 Small-Part Five-Axis Machining: Robot Options and Fixture Access
- CNC Robot Cycle Calculations: Serial Actions, Overlap and an Eight-Second Example
- Robot Unload, Blow-Off and Reload: Separating 90 s Cutting from Handling
Turning and integrated loading
- VL 1 TWIN Bevel-Gear Turning: Pick-Up Spindles and Auxiliary Time
- VT 2-4 and VT 4-4 Shaft Automation: Turret Grippers and Part Limits
- Planetary-Gear Twin-Spindle Turning: A 24-Second Process and 12-Second Output Interval
- XKNC-100GL Small-Part Turning: Pneumatic Handling and Feed Presentation
- Seven KAPP NILES Gear Grinders: Pick-Up Handling and Line Balance
- Printing-Cylinder Bar Feeding: Batch Changeover Versus Part Exchange
- VL 1 TWIN Planetary Gears: TrackMotion and TransLift Transfer
- SHIMADA 2SI Twin Spindles: Indexing Time Versus Loading Time
- RASOMA DS Vertical Turning: Pick-Up Spindles and Sub-Six-Second Handling
- LSCT/N-06 Bar Feeding: Fifteen-Second Bar Change Versus Part Cycle
Workpiece and process evaluation
- TAKISAWA TT-500GD: Dual Loaders and the 2.5-Second Loading Figure
- Okuma MS-320H Loading: Overhead Access and the 5.3-Second Example
- Construction-Machinery Arms: Parallel Setup on a Two-Station Gantry Mill
- EMAG VL 2 P Pendulum Turning: Parallel Loading and Tool Availability
- Maus MTV Vertical Turning: Three-Second Process Transition Explained
- EMAG VLC 250 P Shuttle Turning: Assessing One-Second Change Occupancy
- DW200 Opposed Milling for Power-Tool Shafts: Robot Loading Is Optional
- AY513 Railway-Axle Machining: Dual-End Cutting and Loading Retrofit Limits
- K160 Hobbing Automation: Keep Rotor-Shaft and Helical-Gear Cycles Separate
- GXC-25J Automatic Loading: Resolve the Cycle Unit Before Comparing
- STAR-07T Disc-Part Automation: What a Five-Second Claim Does Not Establish
- Differential-Housing Automation: Separate Spherical and Hemispherical Routes
Focused process and timing guides
- Brake-Disc Line Timing: Exchange, Cutting and Output Intervals
- A/C Connector Cells: Distinguishing NV4G Machines from FANUC Robots
- Rear Brake Drum Transfer: Planning the Vertical-Grinding Handoff
- Two Gears in 20 Seconds: Calculating Parallel-Spindle Output
- Differential Housing Route Selection: Spherical versus Hemispherical Parts
Equipment illustrations
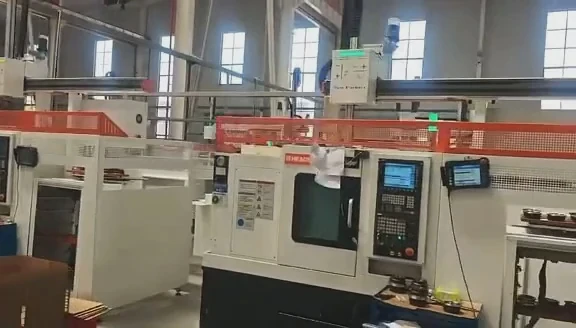
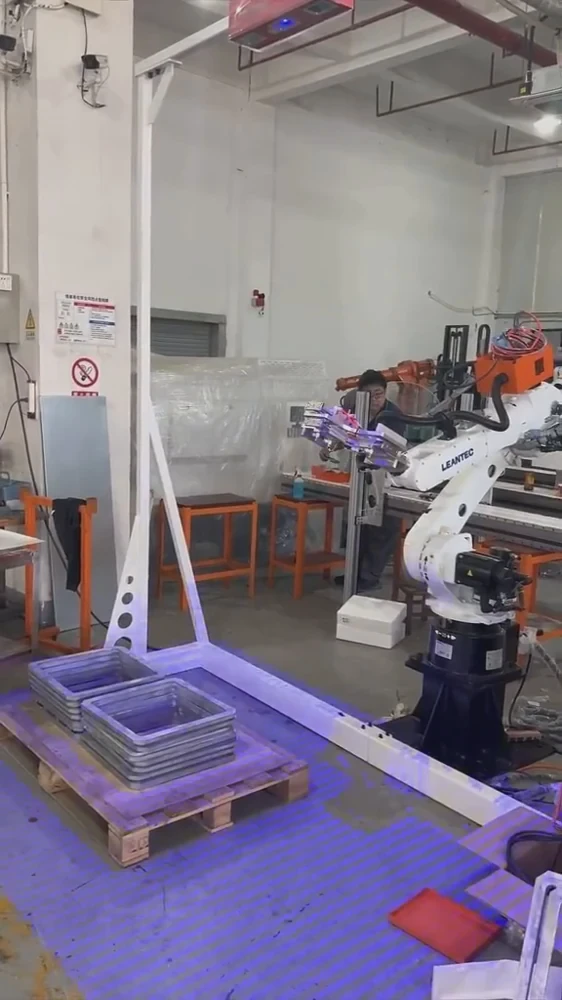
The following images show handling equipment from the available local media collection. They do not document the third-party reference installations discussed in this library.
Prepare an application assessment
Provide the workpiece drawing, blank and finished-part dimensions and mass, machine make and model, process sequence, batch mix, target output and acceptance conditions. Confirm guarding, interlocks, fixture access, chip removal and operator recovery requirements for the proposed installation.
- CNC lathe automation solutions
- Machining-center automation solutions
- Discuss your part and machine configuration
Send the machine brand/model, part drawing or photo, blank and finished-part handling, single or multi-machine layout, target cycle and acceptance requirements.
Request an assessment Call +86 150 5020 2625